It’s time to move beyond coal.
Transforming the green sand moulding process with next-generation additives.
For decades, sea coal has played an important role in green sand moulding. But the framework is changing. Emission requirements, raw-material availability, handling, waste management and economic pressures are creating new challenges for foundries.
HA Green Sand Additives provide new options for moving beyond conventional coal-based systems, from a coal-free hybrid approach to fully inorganic technology.
Why the green sand process needs to evolve
Emissions & Compliance
BTEX, TVOC, TOC, dust and other emissions are increasingly relevant for foundries.
Raw material availability
Availability and consistency of suitable sea coal are becoming an increasing concern.
Safety & Handling
Coal-based systems bring dust, storage, fire and explosion considerations.
Process & Quality
Any alternative must perform under real foundry conditions.
Cost effectiveness
The relevant question is not simply product price, but overall process economics.
ECOSEC at a glance
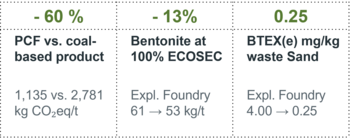
Low carbon (LC) additive without sea coal
- No ATEX certification required and no significant self-heating
- Can be used alone, in addition to bentonite or as a premix; separate dosing increases flexibility compared to a solid premix.
- The addition rate can be reduced by up to approximately 15% compared to coal dust.
- Improved green sand properties: mechanical strength, lower moisture content and reduced bentonite requirements.
- Reduction of TOC and BTEX levels in waste sand as well as improved landfill performance.
PURFORMA at a glance
A new benchmark for low-emission green sand moulding
Inorganic additive
- Non-flammable, non-dust-explosive and not classified as a hazardous material under ADR 4.2.
- Used as a pure additive or with bentonite as a premix; dosing/transport via existing customer equipment.
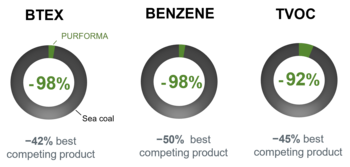
- BREF-based positioning: BTEX and TVOC limits for green sand can be addressed depending on the core sand.
- Application limitations: slightly higher sand adhesion; good unpacking and blasting techniques are preferred.